Introduction
Have you ever watched a production target slip away and asked, “Where did we lose control?” I see this daily on shop floors when a single CNC turning and milling machine hiccup cascades into missed shifts, overtime, and frustrated teams. Picture this: a mid-size cell reports 12% unplanned downtime, scrap rising by 6% year-over-year, and throughput goals that never quite land—what do you fix first? (Hint: it’s rarely the spreadsheet.)
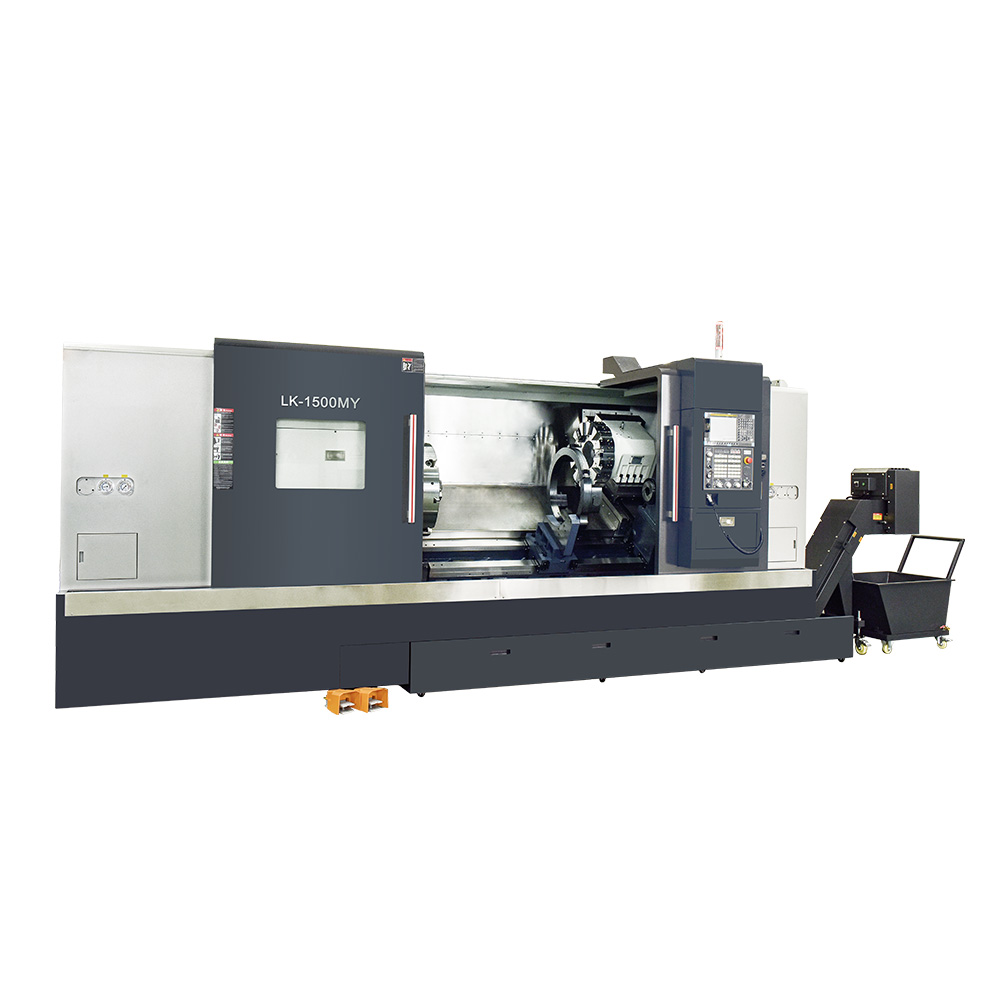
I’m writing from the shop-level viewpoint: I’ve stood beside operators, tuned parameters, and argued with legacy CAM post-processors. My goal here is practical — show where targets and toolpaths disconnect, point to technical causes, and push toward choices you can measure. We’ll move from symptoms to root causes, then to future-ready principles you can test tomorrow. Next: let’s dig into what usually goes wrong beneath the surface.
Where Traditional Fixes Break Down — Hidden Pain Points
cnc milling and turning setups often get complacent with stop-gap fixes: tweak a feed rate, change a cutter, add overtime. Those moves mask deeper faults. I’ve seen shops chase cycle-time like it’s the only KPI, while tool offset drift, spindle speed instability, and coolant flow variation quietly eat accuracy. As we noted above, a small drift becomes a production shift lost — and yes, that’s measurable in scrap cost and customer calls.
Why do traditional fixes fail?
First, they treat symptoms not systems. A quick feed-rate bump reduces cycle time for one job but raises tool wear on the next. Second, data is siloed: CNC control logs, CAD/CAM offsets, and operator notes live in separate places. No single view means no clear root cause. Third, human factors matter — operators adapt workarounds that make sense short-term but wreck repeatability. Look, it’s simpler than you think: when you don’t align tooling strategy with control logic and maintenance, you pay later — funny how that works, right?
So what’s the technical reality? Live tooling synchronization, tool offset management, and stable spindle control are core. If your process doesn’t monitor these — via real-time signals or edge computing nodes that report anomalies — you’ll be reactive forever. I recommend mapping the workflow: identify where tool data flows (CAD/CAM → post → CNC control), where it stops, and where humans patch it. From there, you can prioritize automation that saves time and reduces errors without stifling operator judgment.
Looking Ahead: Principles for Smarter CNC Cells
Shift the lens from firefighting to architecture. I advocate for new-technology principles that focus on resilient processes and measurable outcomes. In practical terms this means: integrate CNC control logs with CAM outputs, deploy condition monitoring on spindle and toolpaths, and standardize setup procedures so tool offsets are accurate across shifts. When you tie these into a decision layer (edge computing nodes, simple dashboards), you get early warnings instead of late surprises.
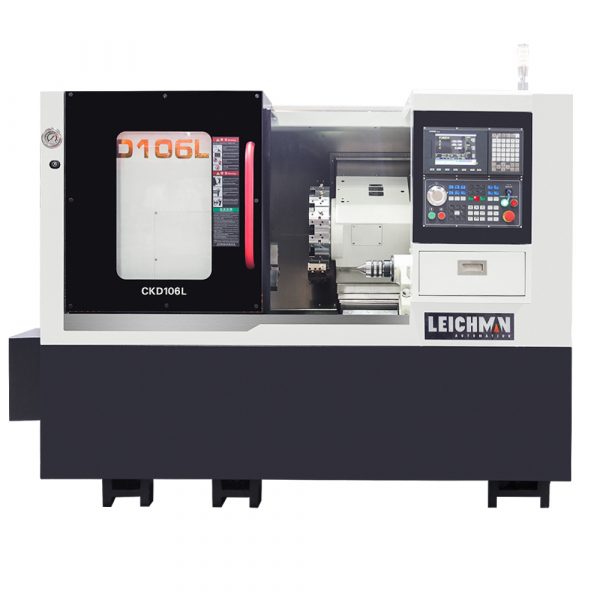
What’s Next for the shop floor?
Implement small experiments: start with one cell and one part family. Add real-time spindle current monitoring and compare against historical profiles; add standardized setup checklists and track first-pass yield. Over time you’ll see clear benefits in uptime and quality — measurable metrics that speak louder than opinions. Also consider power converters and more robust servo tuning if you see electrical noise or torque ripple affecting repeatability.
To help you choose, here are three practical evaluation metrics I use (and you should): 1) Mean Time Between Setup Errors — how often does a setup need correction after initial run? 2) First-Pass Yield Improvement (%) — did your change reduce scrap on first run? 3) Effective Cycle-Time — actual production time per part including non-cutting delays. Use these to judge tooling changes, software upgrades, or workflow fixes. I’ve tried other metrics; these cut through politics and focus on what moves the needle. — they’re blunt, but they work.
We’ve traced the problem from daily pain to practical steps and measurable checks. If you want a turnkey reference machine that supports these practices, consider reviewing the platform options from Leichman — I’m mentioning them because their documented tooling and integration guidelines make experimentation less risky. In short: start small, measure sharply, iterate fast. You’ll find alignment between targets and toolpaths; and you’ll sleep better on Friday nights.